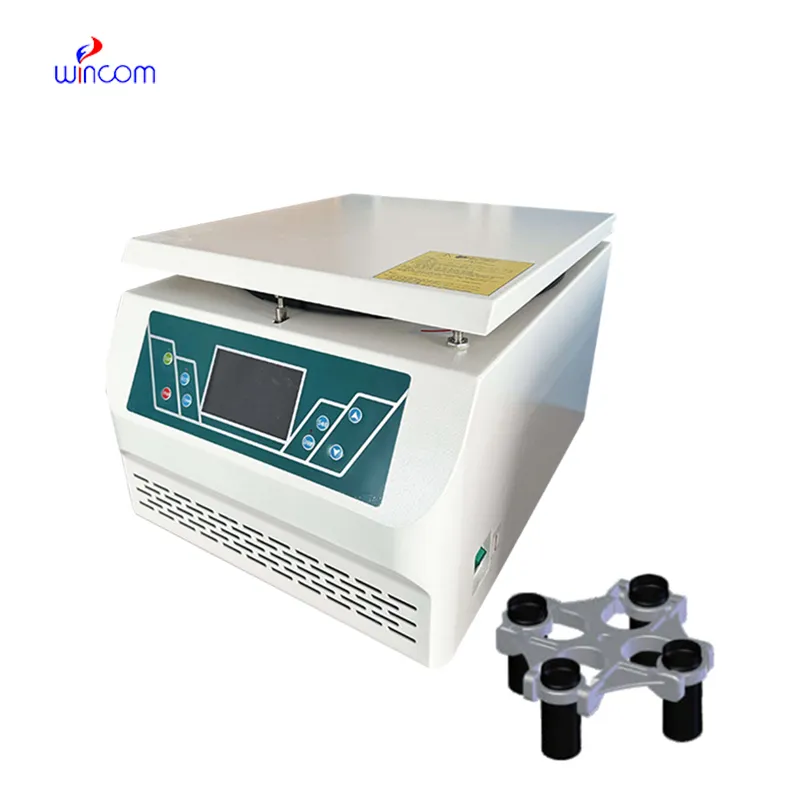
Lightweight yet powerful, the high speed refrigerated centrifuge factory continues to raise the standard for efficiency of operation. High-performance control algorithms provide instant acceleration and smooth deceleration, protecting delicate samples from stress. Dual cooling systems provide thermal stability in even long runs. Modular design provides easy maintenance and upgrading. Remote diagnostics and system optimization connectivity is available in some models. Along with these advancements, the high speed refrigerated centrifuge factory becomes a bridge between traditional engineering and modern automation and functions as a pillar of accurate, high-rate separation within labs and factories around the world.

The applications of high speed refrigerated centrifuge factory span numerous scientific and industrial uses. In medicine, it is used to isolate blood components for transfusion and diagnostic purposes. In molecular biology, researchers use high speed refrigerated centrifuge factory to isolate DNA, RNA, and proteins for genetic studies. The pharmaceutical industry uses it to purify chemicals and enhance the quality of products. Environmental laboratories use high speed refrigerated centrifuge factory to test water and soil samples for contamination. Even in food processing, it aids in the cleansing of juices and the removal of oils. Its applicability ensures consistent outcomes in fields that require careful separation of substances.

The high speed refrigerated centrifuge factory of the future will be innovative, intelligent, and integrated. With the advent of smart manufacturing, high speed refrigerated centrifuge factory systems will operate independently on predictive analytics. Programs with machine learning will interpret vibration patterns to optimize performance with minimal human involvement. Renewable energy integration will make operation more sustainable, and modular design will facilitate instant replacement of parts. Data visualization software will be more sophisticated, providing real-time feedback on the separation process. This blend of mechanical precision and intelligent technology will place high speed refrigerated centrifuge factory at the forefront of international scientific advancement.

Maintenance of high speed refrigerated centrifuge factory is essential to lab safety and data integrity. Cleaning should be performed immediately following every operation, with special attention to the elimination of any liquid spills or residues from samples. The rotor should always be handled gently, placed in an upright position during storage, and never subjected to shock. Periodic inspection of lid locks and gaskets ensures airtight operation. Power cord and fuse conditions should also be checked by operators. Annual servicing by skilled technicians adds lifespan. Through regular care processes, high speed refrigerated centrifuge factory safely and accurately continues to operate.
Scientific and industrial applications use the high speed refrigerated centrifuge factory for its ability to differentiate between mixes with high precision. It relies on the force of centrifugal, which pushes particles off center, leading to density stratification. The method is vital in research, medicine, and engineering. From cell constituents separation to the separation of liquids, high speed refrigerated centrifuge factory make many analytical and production processes easier. Newer models focus on minimizing vibration, maximizing balance, and the use of smart sensors to monitor data in real time. All these advancements have made high speed refrigerated centrifuge factory faster, safer, and more efficient than before.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
The centrifuge operates quietly and efficiently. It’s compact but surprisingly powerful, making it perfect for daily lab use.
We’ve used this centrifuge for several months now, and it has performed consistently well. The speed control and balance are excellent.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Hello, I’m interested in your centrifuge models for laboratory use. Could you please send me more ...
I’m looking to purchase several microscopes for a research lab. Please let me know the price list ...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko