The next generation of super large capacity refrigerated centrifuge systems emphasizes automation, safety, and sustainability. Producers are adding AI-fueled monitoring to predict maintenance needs before mechanical issues arise. Improved rotor dynamics minimize vibration and energy consumption, and closed chambers prevent contamination at high speeds. Touch operation and multilingual interfaces simplify ease of use. In processing biological samples or industrial fluids, the new super large capacity refrigerated centrifuge unites mechanical robustness with digital intelligence, setting the bar higher for precision, productivity, and durability in industrial and scientific applications.

The versatility of super large capacity refrigerated centrifuge can be seen in its application to numerous specialized fields. In marine biology, it helps one analyze plankton and microbial samples. In food science, it helps with the accurate measurement of fat and protein content. The electronics sector employs super large capacity refrigerated centrifuge for purifying liquid crystals and conductive materials. In environmental protection, super large capacity refrigerated centrifuge facilitate tracking of pollutants and studies on recycling. They aid in veterinary medicine in blood diagnosis and disease investigation. With these uses, super large capacity refrigerated centrifuge bring about innovation through offering dependable means for analyzing as well as separating materials.

The super large capacity refrigerated centrifuge technology future lies in automation, digital control, and green engineering integration. Future models will include AI algorithms for speed, balance, and separation efficiency automatic optimization. Energy-efficient motors and recycled materials will reduce environmental impact, following international sustainability goals. Cloud connectivity will allow for remote monitoring and predictive maintenance, with less downtime. In laboratories, super large capacity refrigerated centrifuge will be completely compatible with smart data systems for real-time reporting and process validation. These innovations promise greater accuracy, reliability, and versatility for research and industrial use.

Well-maintained super large capacity refrigerated centrifuge assure trouble-free operation and optimize equipment longevity. Users must ensure balanced loading to prevent excessive stress to bearings. Regular cleaning of the rotor, chamber, and seals reduces cross-contamination. Regular lubrication and calibration ensure mechanical accuracy. Logs of maintenance, checklists, and other records facilitate quality control and inspection for compliance. Internal humidity and dust exposure should be reduced. Laboratories use preventive maintenance instructions to guarantee that super large capacity refrigerated centrifuge delivers constant high performance with little downtime and repair.
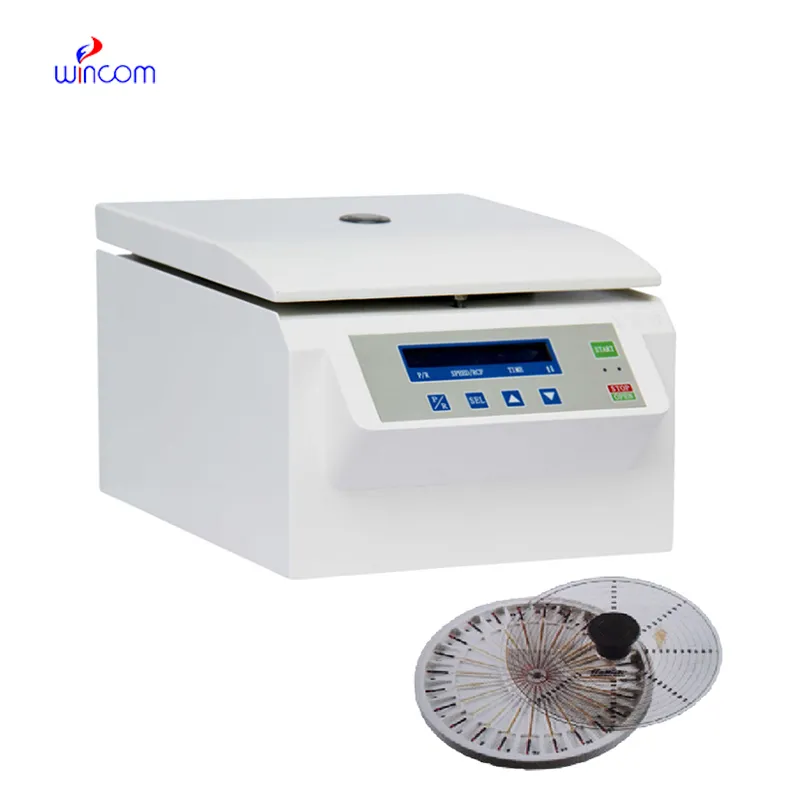
super large capacity refrigerated centrifuge is a piece of mechanical equipment that separates simple mixtures into differentiated parts by utilizing quick spinning. It functions by employing centrifugal force, which expels heavier elements and brings lighter elements closer towards the axis. This principle makes crucial work possible in microbiology, pharmaceuticals, and materials science. High-speed models can achieve exceptional separation accuracy in mere minutes. Modern super large capacity refrigerated centrifuge feature digital interfaces, temperature control, and advanced safety locks to ensure operation. They are so fast and versatile that they are a must-have asset for any laboratory or manufacturing plant.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
The centrifuge operates quietly and efficiently. It’s compact but surprisingly powerful, making it perfect for daily lab use.
I’ve used several microscopes before, but this one stands out for its sturdy design and smooth magnification control.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We are planning to upgrade our imaging department and would like more information on your mri machin...
I’m looking to purchase several microscopes for a research lab. Please let me know the price list ...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko